automation that starts up clean
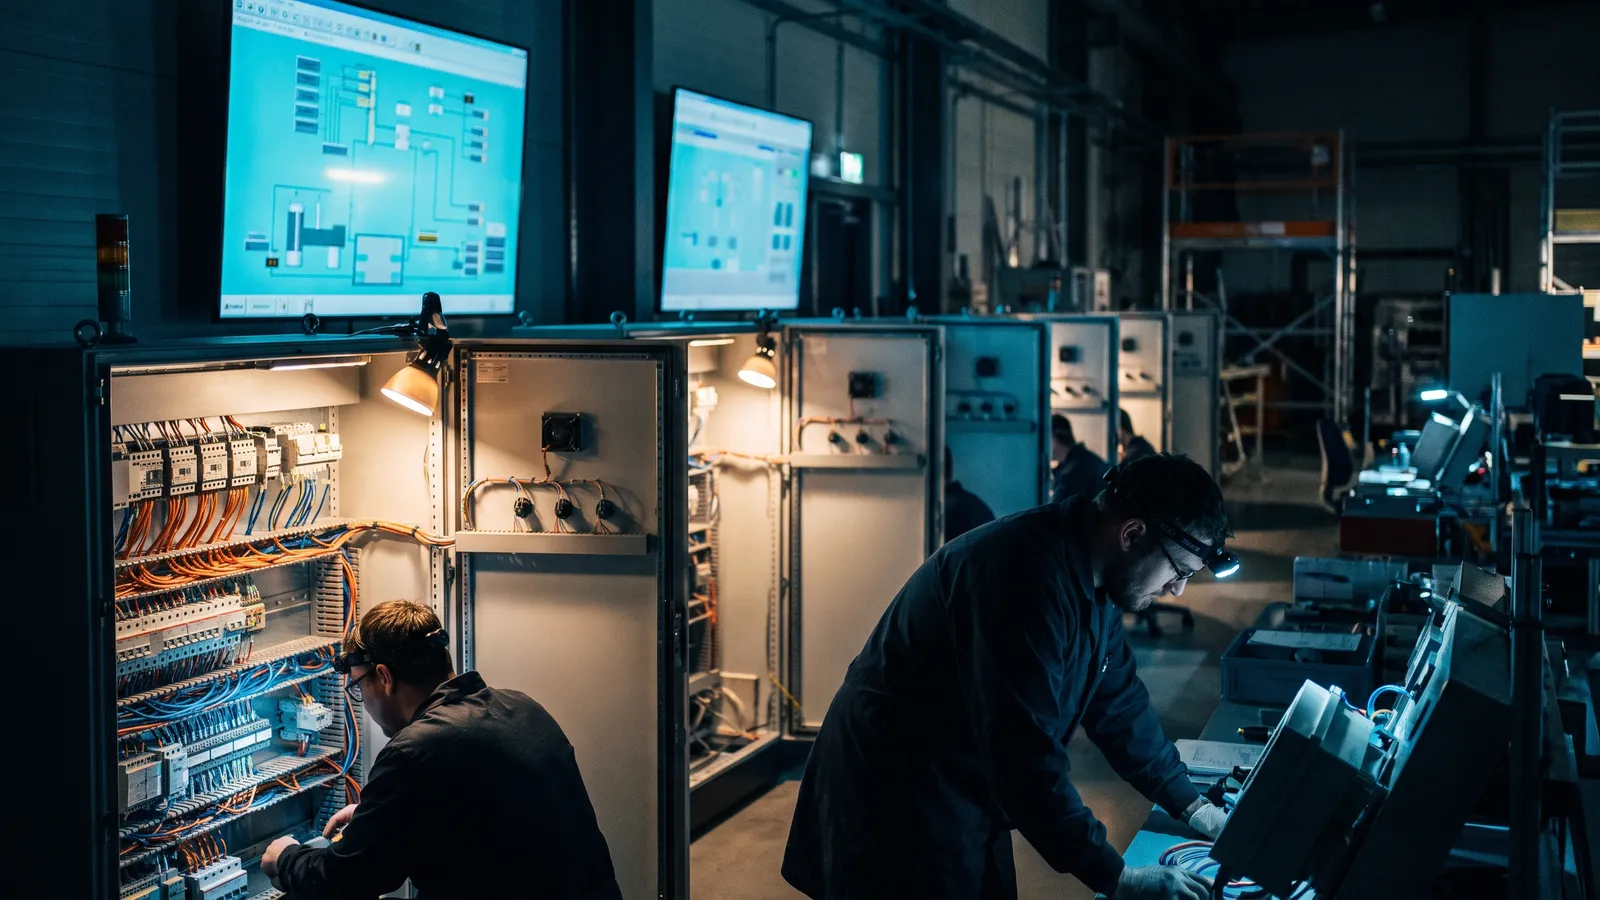
We Build and Program the Panels That Run Your Line
UL 508A control panel fabrication, PLC and HMI programming, SCADA, and robotic work cells for manufacturers across the Southeast.
Do you have a line to automate, upgrade, or migrate?
Get a free scope reviewwhat we do
Specialists in plant-floor automation
One team builds the panel, writes the code, and commissions the line. When something does not behave on start-up, there is nobody to point at and nothing to renegotiate.
Panels
UL 508A Built
Control panels, motor control centres, and operator stations designed and built in our Piedmont shop under a UL 508A listing, with as-built drawings on delivery.
Learn moreControls
PLC and HMI
Ladder and structured text on Allen-Bradley, Siemens, and Modicon platforms, plus HMI development, alarm rationalisation, and documented code you can maintain.
Learn moreSCADA
Data and Networks
Plant historians, OEE dashboards, and industrial networks, including segmented control networks and the reporting your quality group is asking for.
Learn moreRobotics
Work Cells
Pick and place, palletising, machine tending, and vision-guided cells, integrated with the safety circuit, the guarding, and the line that feeds them.
Learn moreOur work
Explore Recent Work
Three projects that show what we mean by a clean start-up: one migration, one new cell, and one plant-wide network.
How we work
Our Core Values
How we work, in the four phrases our customers use when they describe us to somebody else.
One Team Owns It
The people who wrote the code are on site at start-up. No handoff to a subcontractor you never met.
Code You Can Keep
Commented, structured, and documented, with the source handed over. Your electricians should be able to work on it.
Bench Tested First
Every panel is powered and simulated in our shop before it ships, so changeover weekend is installation, not debugging.
Honest Scope
We would rather lose the job at quote than discover the scope gap at commissioning with your line down.
Testimonials
What our customers say
We had been told the PLC-5 migration would take a year of weekends. Kestrel did it in eleven, and we never lost a shift to it. The bench testing is the reason.
What sold me was that they handed over commented source code and the panel drawings without me asking. Our maintenance techs troubleshoot that cell themselves now.
From the field
Latest News
What we are seeing on migrations, cybersecurity, and getting real data off the plant floor.
 ControlsMigration
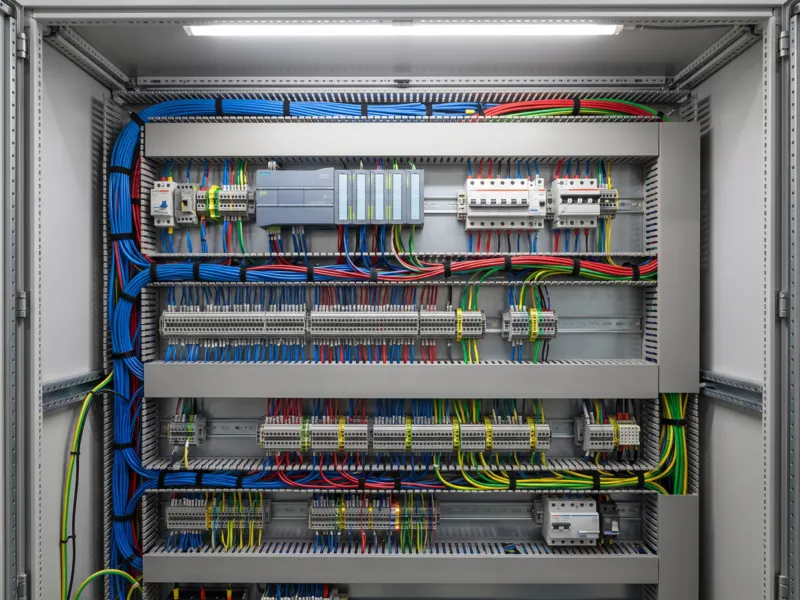
Planning a Legacy PLC Migration Without Losing a Shift
The conversion tool gets you sixty percent of the way. The rest is I/O mapping, timing assumptions nobody documented, and the analog scaling somebody fixed in 1998.
 NetworksSecurity
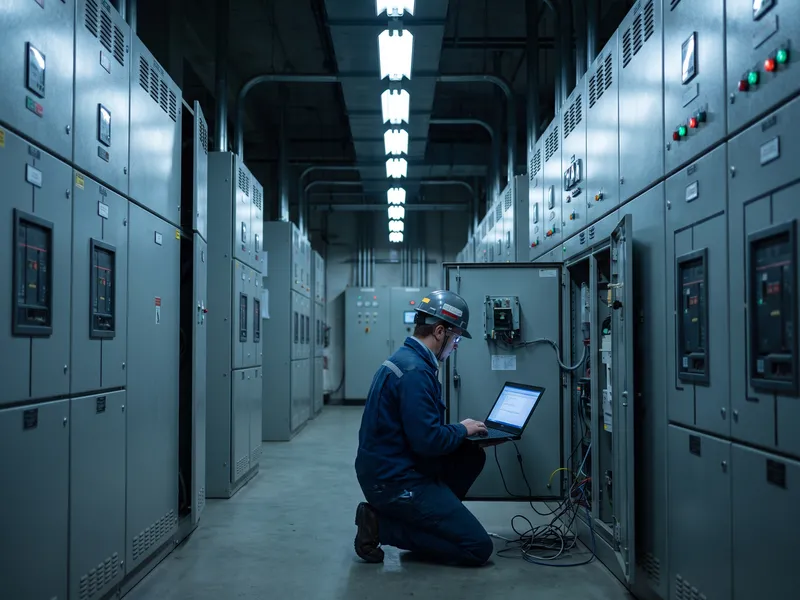
Why Your Flat Plant Network Is a Problem
One broadcast storm from the office side should not stop a production line. Segmentation is cheaper than the downtime and easier than most plants expect.
 SCADAData
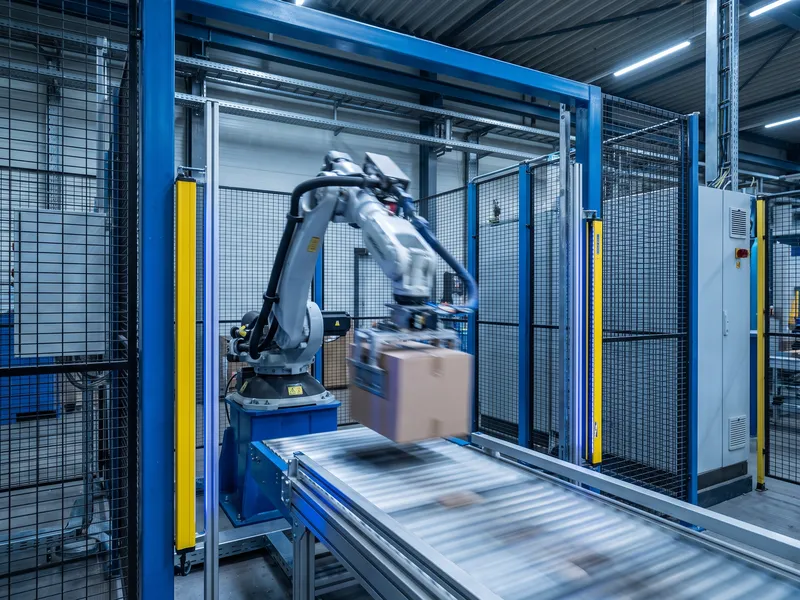
OEE Dashboards People Actually Look At
If the operator cannot see it from the line and the plant manager cannot act on it by Monday, you built a screensaver. Start with downtime reason codes.
Trusted partners
Send us the line you want fixed
Share the platform, the I/O count, and what it has to do. We will come back with a scope, a number, and the changeover plan.
Get a free scope review